
Automation for Machine Shops and CNC Job Shops
Keep spindles cutting when you cannot hire enough operators. We integrate robot and cobot machine tending cells, connect CNCs to real utilization data, and upgrade the controls on the equipment you already own.
The problems we hear from shops
- Not enough skilled operators. Machines sit idle on second and third shift because nobody is there to load them.
- Spindle utilization is a guess. The whiteboard says the machines are busy, but nobody knows the real cut time per shift.
- High-mix work makes automation look impossible. Short runs and frequent changeovers seem to rule out a robot.
- A mixed fleet of controls. Different CNC brands and ages, plus secondary equipment with their own old controllers.
Robotic and cobot machine tending
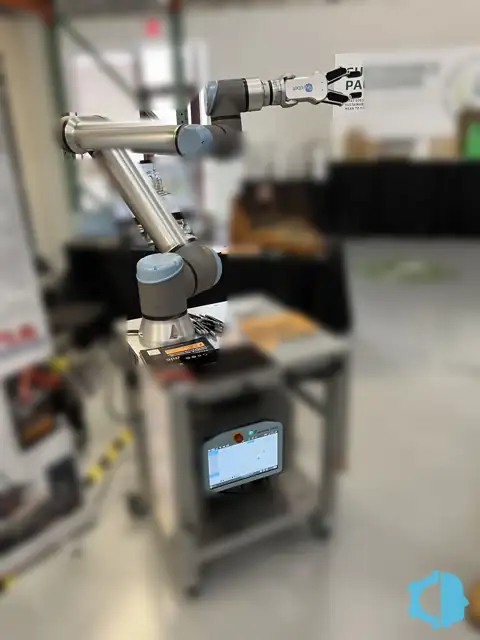
We integrate FANUC industrial robots and Universal Robots cobots to load and unload CNC lathes and mills. The cell design covers how parts are presented (drawers, grid tables, or conveyors), how the robot talks to the machine (door, chuck, vise, and cycle start signals), and how the cell stays safe around people with scanners, guarding, and a documented risk review.
High-mix shops can automate too. The key is designing changeover into the cell from day one: quick-change gripper fingers, part-number recipes saved in the robot and HMI, and fixturing that operators can switch in minutes. The best first candidates are repeat parts with cycle times long enough to let one robot keep a machine running unattended.
Machine monitoring, utilization and OEE
You cannot improve what you cannot see. We pull cycle state, spindle run, alarms, and part counts from CNC controls and PLCs, using MTConnect or OPC UA where the control supports it and simple wired signals where it does not. The result is a live view of every machine by shift, with downtime reasons entered at the machine instead of reconstructed later.
Data is published into a Unified Namespace so the same numbers can feed your ERP, scheduling, and quoting without another custom integration each time.
Controls for secondary and custom equipment
Parts washers, deburr stations, presses, saws, bar feeders, and custom fixtures often run on controllers that are obsolete or undocumented. We program new Allen-Bradley or Beckhoff controls, retrofit aging PLCs, and document the logic so your maintenance team can support it.
How a shop project usually runs
- Floor walk: we look at your machines, part mix, and idle hours to find the cell with the fastest payback.
- Cell design: robot, gripper, part presentation, safety, and changeover plan, with a fixed scope and price.
- Build and test: programming and testing before anything is installed on your floor.
- Commission and train: we run production with your team until they are comfortable changing over on their own.
- Measure: utilization before and after, so you know the payback was real.
Related services
- Robotic and cobot cell integration
- MES integration, OEE and data collection
- PLC programming and controls engineering
Frequently asked questions
Can a cobot tend a CNC machine in a high-mix job shop?
Yes, if changeovers are designed into the cell. Quick-change gripper fingers, grid or drawer part presentation, and saved recipes per part number let operators switch jobs in minutes. Repeat parts with longer cycle times are the best place to start.
Which robots do you integrate?
FANUC industrial robots and Universal Robots cobots, coordinated with Allen-Bradley PLCs when the cell includes conveyors, inspection, or other equipment.
Can you monitor older CNC machines?
Usually yes. Newer controls expose data over Ethernet through MTConnect or OPC UA. Older machines can be monitored with a few wired signals such as cycle start, alarm, and spindle running, brought into a small PLC or I/O module.
Do you work with shops outside the Twin Cities?
Yes. We are based in Big Lake, Minnesota, and work across Central Minnesota, St. Cloud, the Twin Cities, and the Upper Midwest, with remote support for programming changes.
Talk to an engineer
Plantwide Integration is an independent systems integrator based in Big Lake, Minnesota, serving machine shops and CNC job shops across the Twin Cities, St. Cloud, Central Minnesota, and the Upper Midwest. Tell us about the machine or line and we will tell you honestly whether it is a good fit.